Automatic Die Making Steel Rule Die Bender Machine Factory: Precision Manufacturing Insights
2026-10-08
Every fraction of a millimeter counts when a steel rule die meets the press. Yet many converters still struggle with manual bending processes that compromise consistency. At ADEWO, precision isn't a promise—it's built into every automatic die making steel rule die bender machine we manufacture. In this post, we take you inside our factory to explore the engineering insights behind repeatable accuracy, faster changeovers, and reduced material waste. Whether you're scaling up packaging production or refining complex die layouts, understanding what happens on the factory floor could be the missing link in your workflow.
How Precision Bending Shapes Every Die Rule
A die rule only earns its place on the plate when the bend profile matches the intended cut path within a few thousandths of an inch. That level of precision isn't a finishing touch; it decides whether the rule seats cleanly, strips without tearing, and holds its edge through a full run. Even a half-degree deviation at a tight corner can shift where the blade meets the substrate, leaving ragged edges or forcing extra make-ready time on press.
Material choice complicates the picture further. Different rule heights and hardness values spring back at different rates, so a two-point rule bent on the same equipment as a three-point rule will not settle into the same geometry. Skilled operators learn to read that springback almost by feel, adjusting bend angles and dwell times for each batch rather than trusting a one-size-fits-all program. Grain direction in the steel also plays a quiet but stubborn role, especially on shallow-radius bends where the outside of the curve wants to crack or thin.
When the bending process respects these variables, the finished rule drops into the die board with even bridge depths and consistent shoulder contact. That uniformity reduces the need for hand filing and shimming later. It also keeps the cutting edge perpendicular to the sheet, which is the difference between a clean kiss cut and a blade that dulls prematurely or bruises the liner.
Inside the Automated Workflow That Eliminates Manual Guesswork
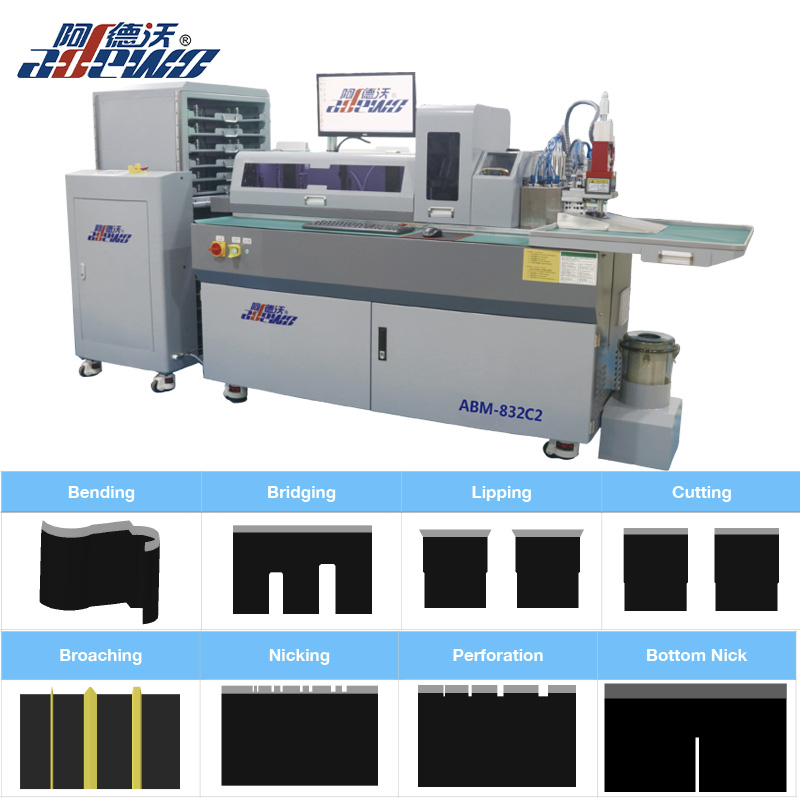
The old way involved staring at a dashboard, trying to decide whether a spike in traffic was real or just noise. Every choice depended on someone's gut feeling, and that inconsistency showed up in delayed responses and uneven results. The automated workflow that replaces it doesn't ask for opinions—it pulls from a set of pre-defined triggers and thresholds that were tuned over months of observation. When a metric crosses a line, the system doesn't wait for a meeting; it executes the next step based on the context it already has.
What makes the difference is not just automation, but the way the workflow layers multiple signals before acting. A single data point rarely triggers anything. Instead, the system checks for confirmation across two or three independent sources—say, a sudden drop in completion rate paired with a rise in error logs. Only when those conditions align does it move to the next stage, whether that's rolling back a change, adjusting a parameter, or flagging an anomaly for review. Manual guesswork used to fill the gaps between those signals; now the gaps are handled by logic that has already learned from past false alarms.
The most noticeable shift is in how the team spends its time. Instead of debating what might be happening, they start from a known state—the workflow has already ruled out the obvious false leads and highlighted exactly which condition was met. That doesn't mean human judgment disappears; it just gets applied where it matters, on exceptions the logic hasn't seen before. Over time, the workflow gets tighter because each override becomes a new rule, and the next time a similar situation appears, the system handles it without anyone having to guess again.
Material-Specific Bending Without Compromising Rule Integrity
Bending stock to a tight radius usually means accepting that the material will thin, crack, or spring back unpredictably. The rule of thumb has long been that you either choose a bend-friendly alloy or accept a compromised bend. This approach ignores the fact that different materials respond to force in fundamentally different ways: aluminum work-hardens quickly, stainless steel resists deformation until a threshold, and mild steel forgives overbending. Treating them all with the same bend allowance tables and the same punch radius is how perfectly good sheet ends up as scrap. A better starting point is to map the specific elongation limit, grain direction, and springback factor of the material before the first hit.
The trick is to adjust the tooling and the bend sequence per material, not to force every material into a generic setup. For example, a 5052 aluminum part bent across the grain can take a much smaller inside radius than the same part bent with the grain, while 304 stainless may need a larger die opening and a few degrees of overbend to land at the target angle. None of this means weakening the bend or cheating the engineering intent. It means reading the material's own limits and working inside them. That way the final bend still meets the print's tolerance for angle, radius, and surface quality, but the scrap bin stays empty.
There is also a habit in some shops of using one set of bend deductions for everything, then blaming the material when dimensions drift. That habit breaks down the moment you switch from hot-rolled to cold-rolled, or from a domestic mill to an import with a slightly different temper. The rule integrity you want to protect is the actual requirement on the drawing — the final formed shape, the hole positions after bending, the minimum inside radius. How you get there can change as long as the end result holds. By treating material-specific behavior as data rather than nuisance, you can hold tight radii, avoid cracking, and still deliver a part that measures correctly without adding a secondary straightening or hand-finishing step.
Meeting Tight Tolerances Across Packaging and Printing Applications
In packaging and printing, a fraction of a millimeter can mean the difference between a flawless run and a costly pile of waste. Substrates shift, inks spread, and cutting dies wear down—each variable threatens the consistency that converters and brand owners demand. Meeting tight tolerances here isn't about chasing perfection for its own sake; it's about keeping every carton, label, and flexible pouch functionally identical, from the first impression to the millionth.
Modern equipment tackles this challenge through closed-loop monitoring and real-time adjustment. Sensors track register marks, color density, and web tension dozens of times per second, feeding data back to servo motors and ink keys that correct drift before it becomes visible. Yet hardware alone rarely holds ±0.1 mm across a full shift. Operators learn to read subtle cues—a slight change in substrate humidity, a dulling blade, a batch of ink with different viscosity—and make preemptive tweaks that automation cannot anticipate.
The payoff appears downstream. When folding cartons align perfectly on high-speed filling lines, when shrink sleeves scan without a single rejection, when flexible packaging seals with uniform lap widths, the entire supply chain feels the benefit. Tight tolerance control reduces material scrap, shortens setup times, and prevents the sort of field complaints that erode customer trust. It's a quiet discipline, but in a market where one misregistered print can halt a promotional launch, it earns its keep every single day.
What Factory-Level Quality Checks Actually Look Like
On a real factory floor, quality checks start before a single unit gets assembled. Incoming materials are sampled against the bill of materials, and a designated inspector logs hardness, thickness, or surface finish using calipers or a profilometer. First-article inspection follows: after the first pieces come off a new run, they are measured point by point against the drawing, not just eyeballed. Operators keep a physical reject tray at each station, and any part with a burr, short shot, or off-spec dimension goes in it, not back on the line. Those trays get counted at shift change, so a spike in rejects points to a specific cavity, tool, or batch rather than a vague quality issue.
Beyond the line, audit tables handle sampling to AQL levels that depend on the customer and part risk. A dimensional layout might use a CMM for critical bores and a height gauge for flatness, while cosmetic checks rely on defined viewing distance, lighting angle, and accepted defect size printed on a visual standard board. If a measurement drifts near a control limit, the process gets adjusted before parts fall out of spec. For high-risk items, a small batch may be pulled for torque testing, leak-down, or cross-sectioning. Every nonconformance is tagged with a physical red tag and logged with photos, corrective action owner, and a due date, because a factory quality check is not a sign-off, it is a recoverable record of what was actually verified.
Custom Rule Profiles for Non-Standard Die Designs
Non-standard die designs rarely fit the assumptions baked into default rule sets. A deep draw with an asymmetric flange, a multi-gate family mold with widely varying wall thickness, or a die insert that must survive abrasive fillers—each of these breaks at least one generic guideline. Custom rule profiles give designers a way to encode the specific limits that matter for these outliers, instead of forcing every check through a one-size-fits-all filter.
A profile typically starts with a baseline standard, then layers on overrides for selected geometry, material, or process conditions. For example, a profile might allow draft angles as low as 0.5 degrees on textured sidewalls but require 3 degrees on polished surfaces, or it might flag wall thickness transitions only when the ratio exceeds 1.8:1 rather than the usual 1.2:1. These rules are stored alongside the part or die model, so the same exceptions apply every time the design is validated—not just when the original engineer happens to remember them.
The payoff shows up during design reviews and handoffs. Instead of debating whether a non-standard feature is acceptable, the team can point to the active profile and see exactly which rules were relaxed and why. That cuts down on rework, preserves tribal knowledge, and makes it easier to onboard new engineers onto complex tooling programs without watering down the rigor of the standard checks.
FAQ
Precision die making hinges on repeatability. An automatic bender removes the subtle variations of hand bending, so every rule segment follows the programmed angle and length exactly, which matters when a cutting die must match a design within a few thousandths of an inch.
Manual bending relies on operator feel and can drift with fatigue. Automatic systems use servo-driven axes and closed-loop feedback, so the same bend command produces the same result on the first rule and the thousandth. That consistency directly cuts scrap and speeds up die assembly.
A factory needs to control temperature, keep tooling sharp, and verify machine geometry daily. Even a small misalignment in the bending head or a dull punch will show up as angle error, so regular checks with a protractor or laser measurement keep tolerances from creeping.
Steel rule hardness and thickness dictate the bending force and minimum radius. Softer rule bends easier but may deform under cutting pressure, while harder rule holds an edge longer yet needs more careful handling to avoid micro-cracks at tight bends. Factories match the bender settings to the exact alloy and temper.
Software translates CAD die layouts into bend sequences and compensates for springback automatically. Instead of an operator calculating each angle, the program stores material profiles and adjusts in real time, which lets the machine handle new designs without trial bends.
Yes, but complexity comes at a cost in cycle time. Multi-axis benders can rotate and tilt the rule between bends to create intricate profiles, yet sharp internal corners and very tight radii may still need a secondary hand-finishing step. The machine handles the bulk of the geometry accurately, leaving only rare exceptions.
One common problem is springback variation between steel batches. Factories counter it by testing each new coil and updating the bend compensation file. Another issue is tool wear on high-volume runs; scheduled micro-adjustments on the punch and die keep angles within spec rather than waiting for a visible defect.
Calibration ties every movement to a known standard. Over months, ball screws, belts, and sensors drift slightly, and without routine calibration the machine will confidently produce wrong angles. A weekly check against a certified angle block or laser interferometer catches drift before it becomes scrap.
Conclusion
At the core of an automatic steel rule die bender machine factory lies a direct relationship between bend accuracy and the final performance of each die rule. Precision bending does more than shape metal—it determines how cleanly the rule will cut, crease, or perforate later on. The automated workflow removes manual guesswork by relying on sensor-guided angle control and repeatable motion profiles, so every bend lands within the intended geometry without operator-dependent variation. This becomes especially critical when handling different rule materials, because each alloy or hardness level responds differently to force and speed. Adjusting parameters per material keeps the rule's structural integrity intact, avoiding micro-fractures or spring-back that could weaken the cutting edge over long production runs.
In packaging and printing applications, tight tolerances are not optional; a deviation of a fraction of a millimeter can cause misregistered folds or incomplete cuts. Factory-level quality checks step beyond basic visual inspection, using automated measurement stations that compare each bent profile against its CAD reference before the rule leaves the production cell. For non-standard die designs, the system supports custom rule profiles that store unique bend sequences, angles, and offsets, allowing short-run or unusual shapes to be produced with the same confidence as high-volume standards. These combined capabilities mean the factory can maintain both speed and accuracy across a broad spectrum of die-making demands without sacrificing repeatability.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com